Computer vision in manufacturing: use cases that pay off
By Graeon.ai · Updated
Short answer
Computer vision in manufacturing means using cameras and AI to see what is happening on the shop floor in real time. The use cases that pay off fastest are safety compliance, quality inspection, process and material tracking, gate and vehicle automation, and workforce attendance — because each replaces a manual check that happens too rarely or too late.
Safety compliance
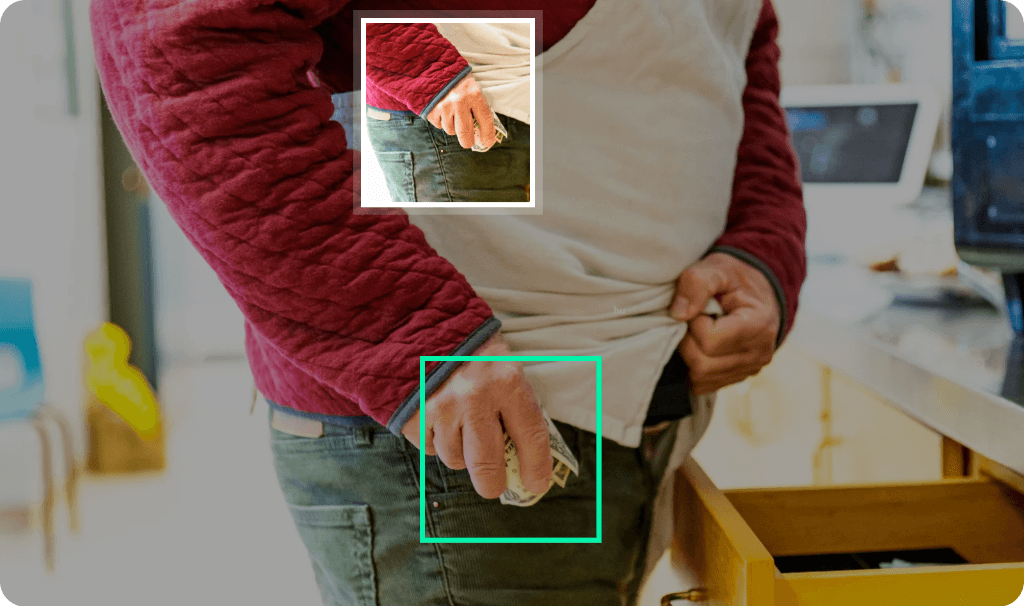
Helmet and PPE detection, zone breach alerts, slip-and-fall and heat-and-smoke detection, with customisable rule sets per area.
Quality inspection
AI image analysis spots cracks, scratches and other defects on the production line, and checks that SOP steps are followed.
Process and material tracking
Track critical operations such as ladle loading and turnaround, material movement between zones, loading bay utilisation, and finished goods yard activity.
Gate and vehicle automation
ANPR cameras automate boom barriers and vehicle gate passes and flag entry-exit mismatches and gate pass fraud.
Workforce and manpower
Face recognition attendance for permanent and contract workers, manpower mapping across zones and shifts, and idle-time detection, linked to payroll and Factory Act registers.
Why connecting it to ERP matters
Detections become far more valuable when they update the systems that run the plant. Graeon connects shop-floor vision AI with ERP modules for manufacturing, inventory and compliance, so plant managers see live production, manpower and equipment status in one dashboard.